The company
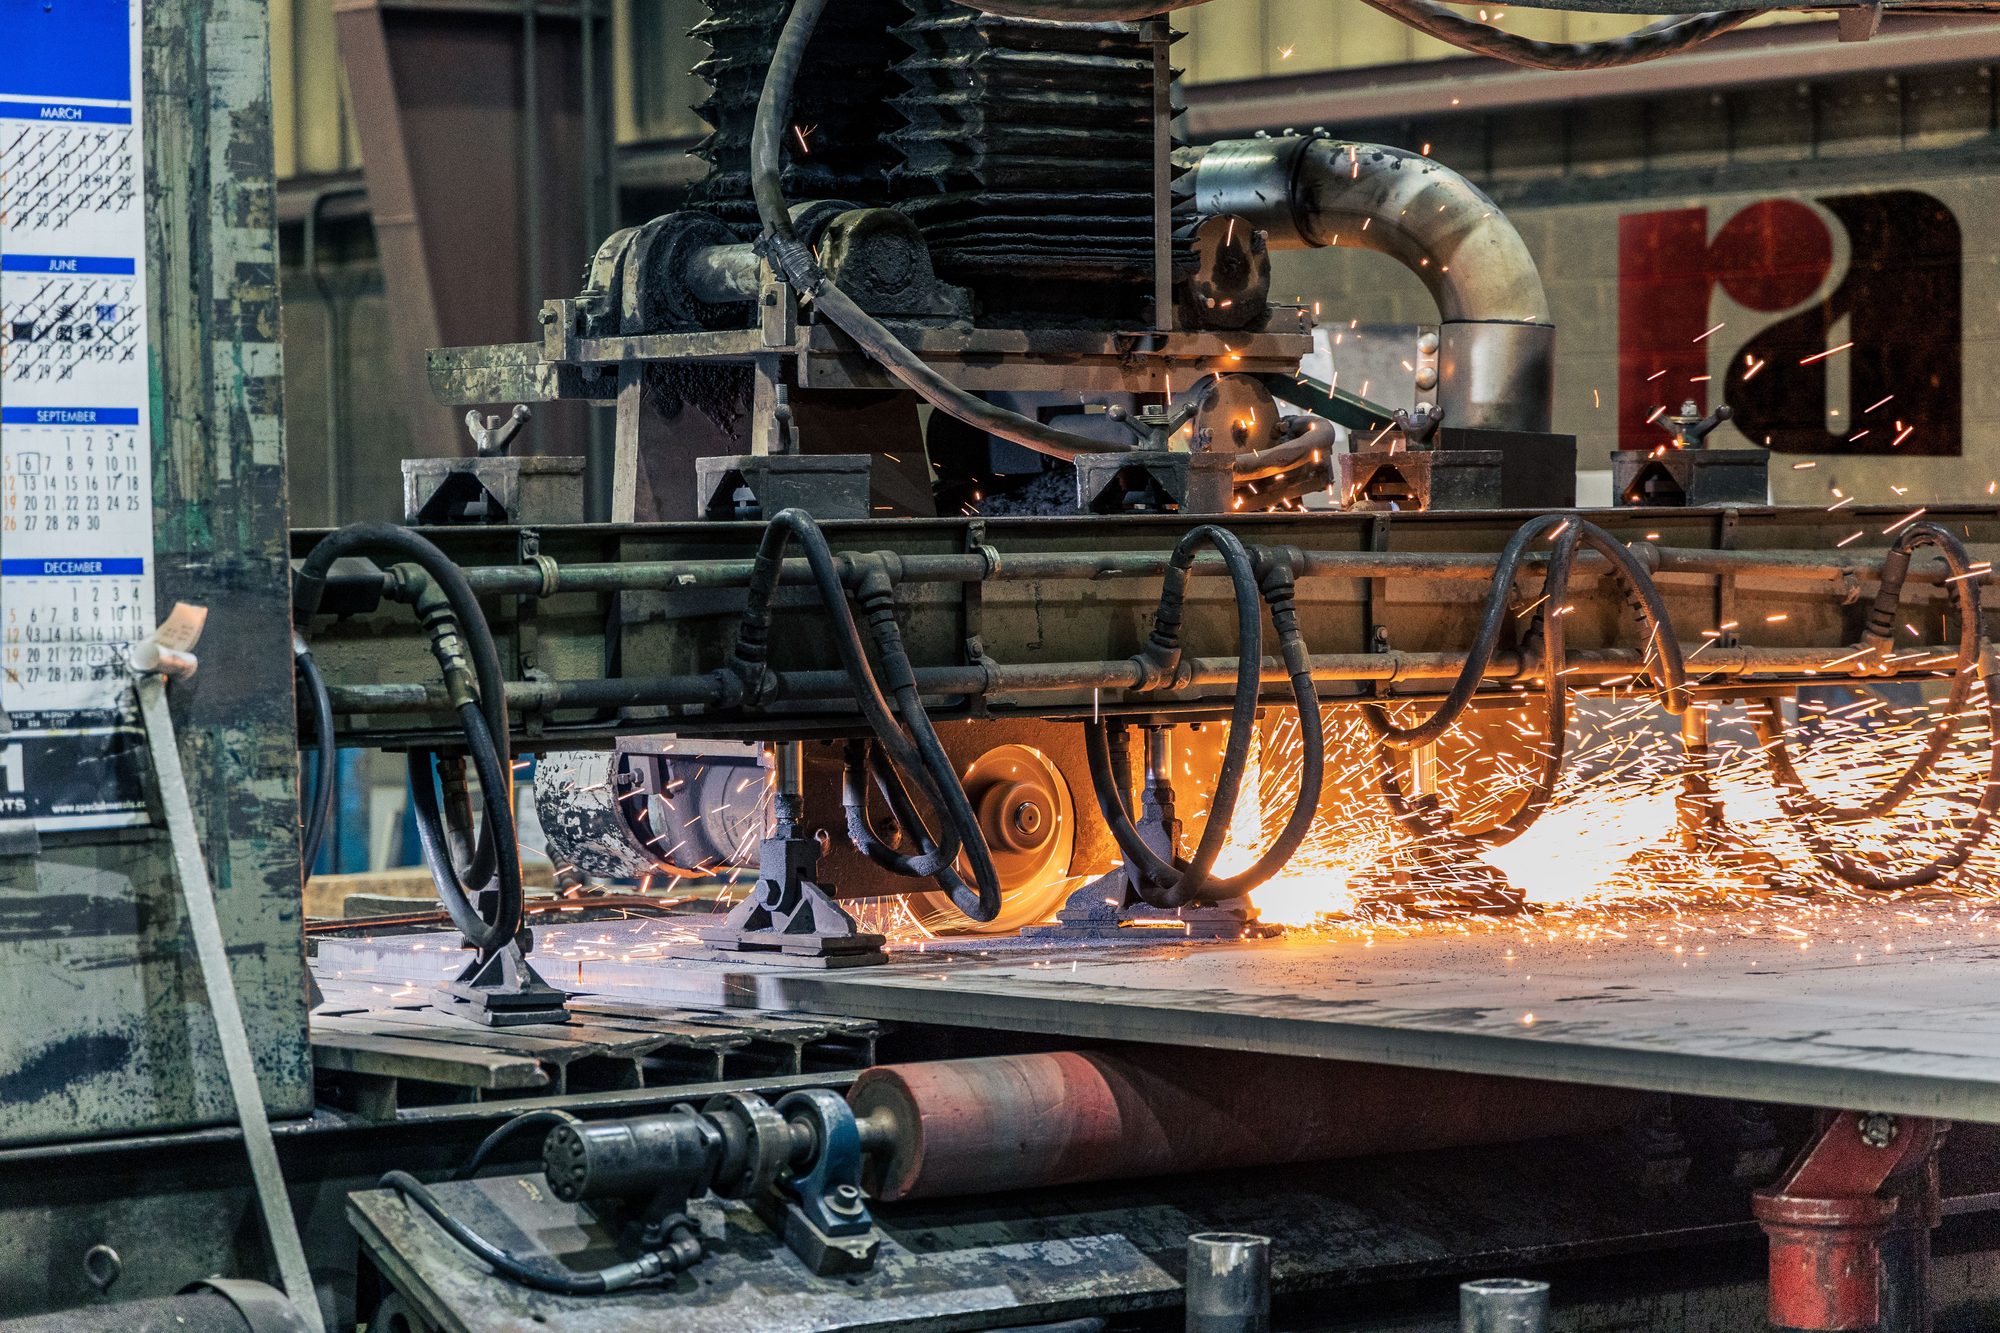
A steel foundry at GIDC Savli, Vadodara, making high manganese and alloy castings for equipment that runs hard.
Founded on metallurgy, grown on capacity.
Baroda Hi-Tech Alloys Pvt. Ltd. was set up in 1994 to give mining and quarrying customers in western India a local source of Hadfield manganese wear parts.
Thirty years later the plant runs three induction furnaces, two solution annealing furnaces and its own machine shop across 18,500 square metres at GIDC Savli. Production capacity has grown by more than 100% since 2019, on the back of the 3,500 KW furnace and a second heat treatment line.
The leadership and technical team carries over 150 years of combined experience in melting practice, sand systems, heat treatment cycles and the inspection regimes that critical wear parts demand.
Three things we hold to.
Full process ownership
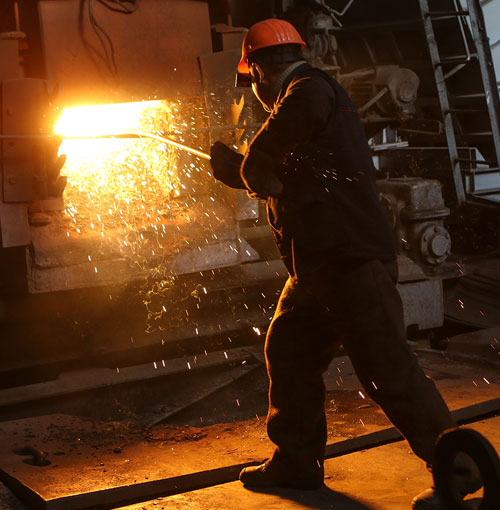
Melting, moulding, heat treatment, fettling and machining are all ours. When a delivery date slips it is our problem to solve, not a sub-contractor's to explain.
Metallurgy you can audit
Chemistry is verified on every pouring heat and the heat treatment chart travels with the casting. If a part fails in service we can trace it back to the furnace that made it.
Honest lead times
We quote against the pattern shop and furnace load we actually have. A longer date that holds is worth more to a maintenance planner than a short one that does not.
Capacity, added when a bottleneck demanded it.
Each step below came out of a constraint we had hit, not a target we had set. Installed annual tonnage is shown where recorded.
-
1994
First heat
The company is founded at Vadodara with a single 500 kg induction furnace and a hand-rammed green sand line, supplying jaw plates to local quarries.
400 MT -
1999
Move to GIDC Savli
Operations shift to plots 26 to 28, giving room for a dedicated melting bay, a knockout area and the first on-site heat treatment furnace.
1,200 MT -
2006
ISO 9001 certification
The quality system is formalised and independently certified. Heat-wise analysis and documented heat treatment charts become standard on every despatch.
-
2011
No-bake moulding
An automatic resin sand mixer with PLC control and a 3.5 × 2.5 m vibrating table bring dimensional scatter and surface finish up to export standard. First overseas order follows.
2,100 MT -
2015
750 KW furnace and machining
An Inductotherm 750 KW furnace is installed with 2,000 and 2,500 kg crucibles. Vertical boring, milling and radial drilling come in-house so castings can ship finish machined.
3,000 MT -
2019
15 MT heat treatment furnace
A second solution annealing furnace with six-point recording pyrometry and a matching fork-lift crane removes the constraint on large single-piece castings.
-
2022
3,500 KW furnace
The largest investment in the company's history takes single-heat capacity to 10 tonnes, opening up mill liners and heavy structural work.
6,000 MT -
2024
ZED Gold and 2-Star Export House
The plant is rated ZED Gold by the Quality Council of India. DGFT grants Two Star Export House status on sustained export earnings.
-
2026
Today
7,200 MT of installed capacity, 310 people, customers in 18 countries and 820 kWp of rooftop solar covering a growing share of daytime load. Debottlenecked fettling and a second machining cell.
7,200 MT
Who runs the plant.
Our metallurgists, pattern engineers and inspectors have spent their careers around induction furnaces and no-bake moulds.
Rajendra Mehta
Managing Director
Anjali Desai
Director, Quality
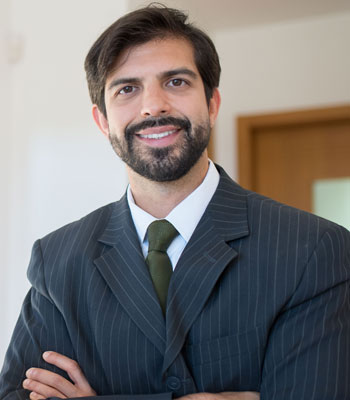
Sunil Patel
Works Manager
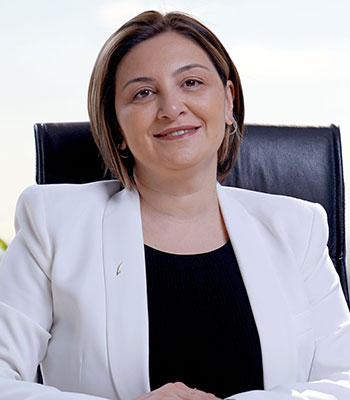
Meera Kulkarni
Head of Metallurgy
We rarely win an order on price. We win the repeat order, when the customer compares how long our casting lasted against what they were running before.
Manganese steel is unforgiving. Fifteen seconds late into the quench and you have made an expensive paperweight. That is why the furnace charts are not negotiable here.
Come and audit the plant.
Melting, moulding, heat treatment and the laboratory are open to customers and prospective customers. Call ahead and we will arrange the day.